The short answer: vet a custom toy manufacturer on seven verifiable dimensions — in-house sculpting capability, tooling ownership, QC infrastructure, IP/NDA controls, capacity math, certification scope, and project management. Ask for the physical evidence behind each, not the marketing claim. The two checks that eliminate most unsuitable suppliers fastest are (1) whether they sculpt and cut tooling in-house, and (2) whether they can show you an AQL inspection report from a live project.
Sourcing a custom toy or collectible figure is not the same as buying a stock product. You are commissioning a tool, a paint specification, a packaging format and a compliance file — and those assets only pay off if the supplier behind them is real. A manufacturer that outsources sculpting, then outsources tooling, then assembles in a rented workshop creates three failure points where your budget and your schedule can disappear.
This guide sets out a vetting framework you can run in two rounds: a desk review first, then a factory visit (physical or video-walked). Every item below is something a serious manufacturer can evidence on request. If a supplier deflects on the evidence, that deflection is itself the answer.
In this article
- The seven vetting dimensions at a glance
- Round one: desk review before you talk price
- Dimension 1 — In-house sculpting and engineering
- Dimension 2 — Tooling ownership and mould capability
- Dimension 3 — QC infrastructure and AQL discipline
- Dimension 4 — IP security and NDA controls
- Dimension 5 — Capacity math, not capacity claims
- Dimension 6 — Certification scope and test reports
- Dimension 7 — Project management and reporting cadence
- Scoring the seven dimensions
- Red flags that should stop the conversation
- FAQ
The seven vetting dimensions at a glance
Before drilling into each dimension, here is the framework in one table. The right-hand column is the evidence you should actually request — a claim without a document behind it should be treated as unverified.
| Dimension | What you are really testing | Evidence to request |
|---|---|---|
| 1. Sculpting & engineering | Can they translate your 2D concept into a production-ready 3D asset without a third party? | Native sculpt files, structural review notes, a sample of approved six-view sheets |
| 2. Tooling | Do they cut and maintain the mould, or resell someone else's capacity? | Mould register with cavity counts, maintenance log, machining centre photos/video |
| 3. QC infrastructure | Is there a measurable inspection process, or only a visual once-over? | AQL plan, inspection report from a live order, calibration records, in-line test equipment list |
| 4. IP security | Can your designs leak? | Signed NDA template, access-control policy, scrap-handling procedure, server/network policy |
| 5. Capacity | Can they hit your quantity inside your window? | Machine count and tonnage, shifts per day, monthly output by product family |
| 6. Compliance | Will the goods actually clear your market? | EN71 / ASTM / REACH / CPSIA test reports with report numbers and dates |
| 7. Project management | Will you know what is happening without chasing? | Sample approval gates, named project contact, reporting template, escalation path |
Why this order matters. Dimensions 1 and 2 are structural — if either fails, no amount of good QC later will rescue the project. Dimensions 3–7 are operational — they can be improved with a management plan. Score the structural dimensions first, and let them gate the rest.
Round one: desk review before you talk price
Most buyers open with "send me your best price." That inverts the process. Price is only meaningful once you know what is being quoted — and the desk review is how you find out. Spend 30 minutes on the following before you engage on commercials.
What the public record tells you
- Product range coherence. A manufacturer that genuinely runs full-cycle model toy and figure production will show a consistent portfolio — scale ranges, material families (ABS, PVC, resin), and finish types that hang together. A patchwork of unrelated goods suggests trading, not manufacturing.
- Process disclosure. Look for named processes with specifics: FREEFORM sculpting, structural engineering in a CAD package, tooling, injection, pad printing, hand painting, assembly. Vague words like "advanced technology" carry no information.
- Named capability numbers. Facility area, machine types, annual output, on-time rate. These are checkable claims — and the fact that a manufacturer publishes them is a mild positive signal.
- Named clients or sectors. Reference to established brand relationships (toy majors, anime merchandise, promotional gift programmes) is worth more than a logo wall of unverifiable marks.
The enquiry that reveals the most
Send a single, specific technical question rather than a general brochure request. For example: "We are developing a 12 cm collectible PVC figure with a two-part body and a separate display base. Can you advise on the likely tooling structure, and what undercut risks you would want to resolve during the sculpt review?"
The quality of the reply separates real manufacturers from intermediaries within one email. A real factory will answer with structural specifics — parting lines, draft, undercut handling, base attachment. An intermediary will reply with a price range and a promise to "check with the factory."
| Reply pattern | What it indicates | How to proceed |
|---|---|---|
| Structural specifics: parting lines, draft angles, undercut strategy, material grade | In-house engineering with production experience | Proceed to Round two |
| Questions back to you: wall thickness, target market, expected annual volume, licence status | Experienced project intake — they know what drives cost | Proceed to Round two |
| Price range plus "we can do anything" | Trading company or unqualified workshop | Request factory walkthrough video or decline |
| No technical content, only MOQ and lead time | Sales-driven front end | Request direct contact with the technical team |
Dimension 1 — In-house sculpting and engineering
This is the single most predictive dimension. If the supplier cannot sculpt and engineer in-house, every design revision becomes a negotiation with an unknown third party, and your schedule becomes someone else's queue position.
What in-house actually means
"In-house sculpting" should mean the manufacturer employs sculptors and engineers who produce the 3D asset themselves, in a format that feeds directly into tooling. It should not mean sending your concept to a freelancer and forwarding the result.
- Ask which sculpting software is used natively. For organic collector figures, FREEFORM is a common choice; hard-surface and mechanical parts often run through a parametric CAD package. A manufacturer should be able to tell you which tool they reach for, and why.
- Ask for a six-view approval pack from a past project. A disciplined studio produces front, back, left, right, top and bottom views for client sign-off before tooling starts. If the pack does not exist, the approval gate is informal — and informal gates are where expensive rework hides.
- Ask how undercuts are resolved. The answer should reference parting-line placement, the use of inserts or sliders, and whether the resolution affects the visual silhouette. This is a technical conversation a trading company cannot fake.
Verification test: request a ten-minute screen-share of the sculpt file itself — not a rendered image, but the actual working model in the sculpting environment. A manufacturer with genuine capability will show you layer structure, retopology notes or measurement overlays. A reseller will send you a JPEG.
Dimension 2 — Tooling ownership and mould capability
Tooling is the highest-risk line item in any custom toy budget. It is paid up front, it is not recoverable if the project stops, and it is the item most often subcontracted without the buyer's knowledge. Two questions settle it.
Who cuts the tool
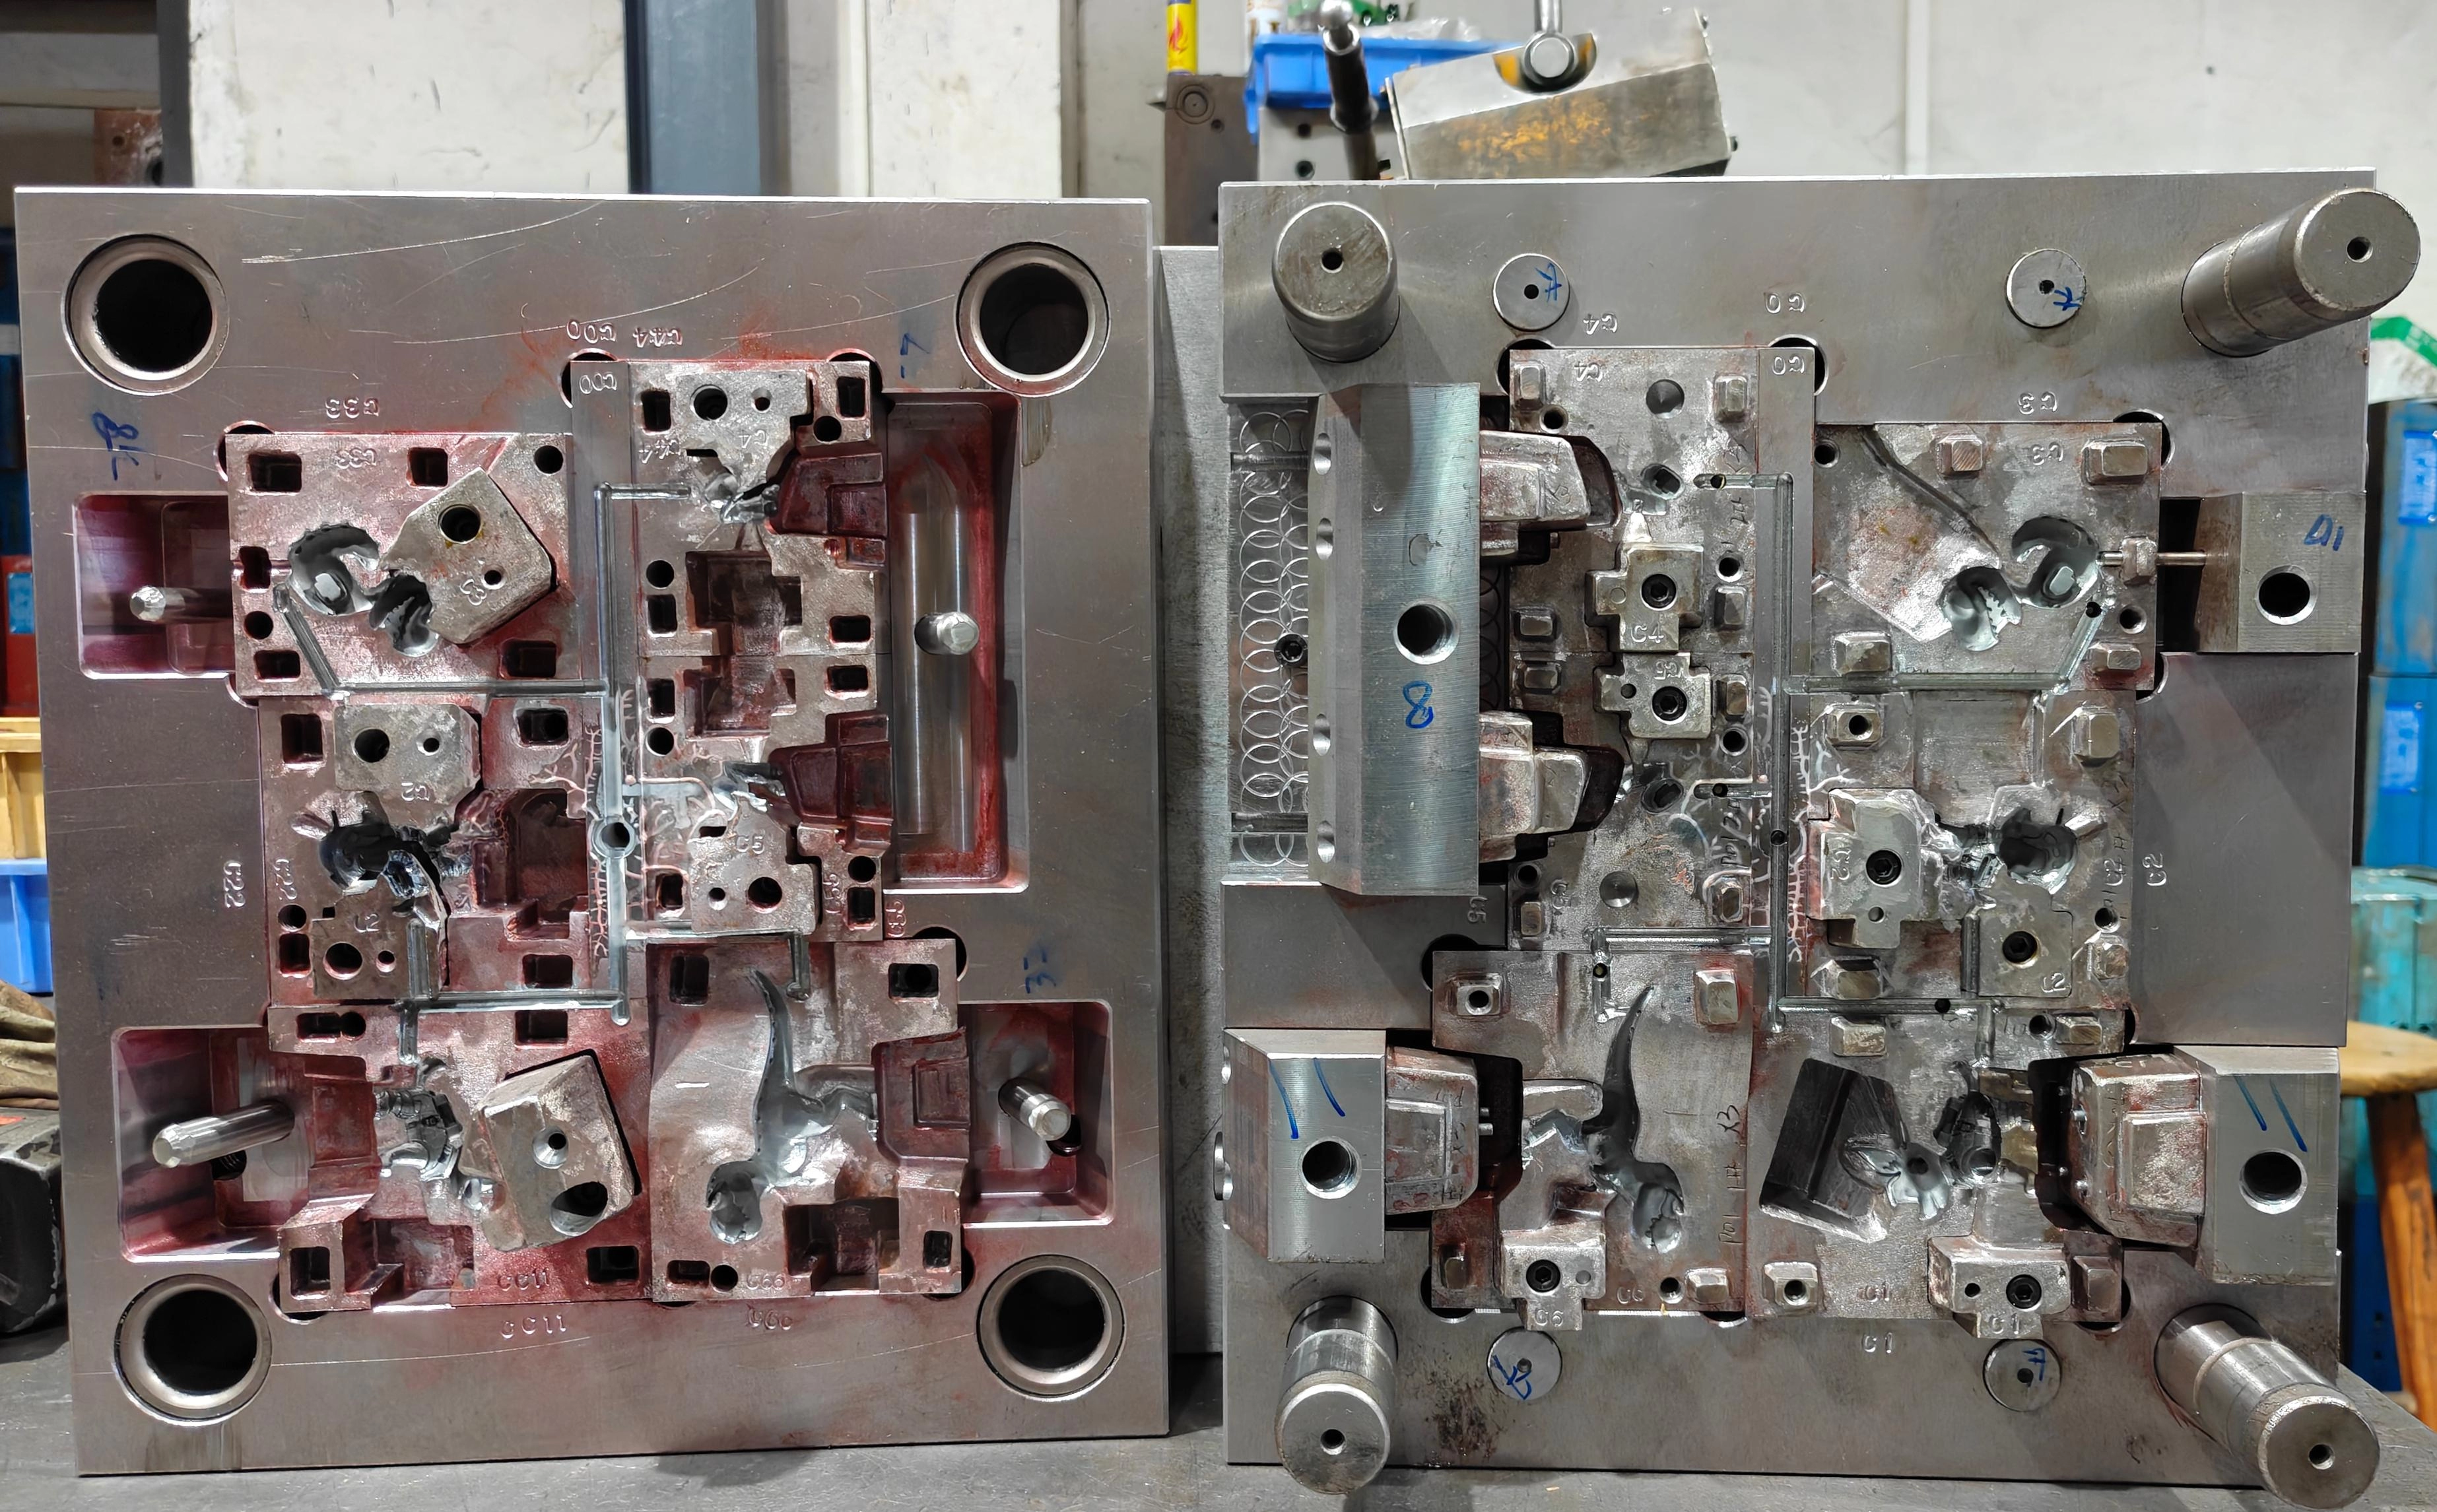
A manufacturer with an in-house tooling cell runs CNC machining centres on site. Ask for the machine list with tonnage and axis count, and ask for the mould register — the internal log of every tool including cavity count, steel grade, and the project it belongs to. A factory that cuts its own tools keeps a register. A reseller has no register because it has no tools.
| Tooling question | Good answer | Warning answer |
|---|---|---|
| Where is the mould cut? | On site, with named machining equipment and a tooling cell headcount | "Our partner factory handles tooling" |
| How many cavities does the tool have? | A specific cavity count tied to your volume forecast and unit economics | Vague: "however many you want" |
| Who owns the tool? | Buyer pays, buyer owns; ownership documented in the PO or a separate tooling agreement | Silence, or an assumption that the factory retains the tool |
| What is the tool life? | A stated shot count with steel grade named, plus a maintenance interval | No figure offered |
| What if the design changes after cutting? | A costed engineering-change process with a stated rework or re-cut price | A promise that changes will be handled later |
Tool ownership should be in writing
The commercial agreement should state, explicitly, that the mould is the buyer's property once paid for, and that the manufacturer will store, maintain and — on request — ship the tool to another party. This single clause protects your investment if the relationship ends. It is a normal request; a manufacturer that resists it is telling you something.
Dimension 3 — QC infrastructure and AQL discipline
Quality control in custom figures is not a final inspection — it is a chain. Paint coverage, joint fit, decal registration and colour consistency all have to be controlled at their own step. Ask what happens at each stage, and ask to see the record.
The checkpoints that should exist
| Stage | What is controlled | Record you should be able to see |
|---|---|---|
| Incoming material | Resin/PVC grade, colour batch, additive conformity to the specification | Incoming inspection sheet, supplier batch certificates |
| First-off / first article | Dimensional and visual conformance of the first parts off the tool | First-article report against the approved drawing |
| In-process (moulding) | Shot weight, cycle consistency, flash, short shots, sink marks | In-process inspection log at a stated frequency |
| Paint / decoration | Pantone match, coverage, masking accuracy, pad-print registration | Colour approval against the signed sample |
| Assembly | Joint fit, articulation range, glue/heat-stake integrity, base seating | Assembly line check sheet |
| Final AQL | Sampled inspection of finished, packed goods before cartoning | AQL inspection report with defect classification and lot size |
| Pre-shipment | Carton integrity, labelling, quantity, palletisation | Pre-shipment inspection report and photos |
How to test the claim
Ask for an AQL report from a live project, then check three things: whether the lot size and sample size are arithmetically consistent, whether defects are classified into critical / major / minor, and whether the report names the inspector and the date. A report that is a scanned checklist with no sample-size arithmetic is theatre.
On sampling standards: the widely used general inspection levels are defined in the ISO 2859-1 / ANSI Z1.4 family, with AQL limits typically tightened for critical defects. Ask the manufacturer to state the AQL levels they apply by defect class — a serious factory has a house standard and can quote it from memory.
Also worth asking: whether in-house test equipment exists — for example joint fatigue rigs, drop towers, or tensile testers. A manufacturer that can run a joint-life cycle test before shipping is preventing a problem rather than reporting one.
Dimension 4 — IP security and NDA controls
Your sculpt, your mould geometry, your packaging artwork and your brand assets are the whole project. In licensed and branded collectible work, a leak is not an inconvenience — it can end the programme and expose you commercially.
What a real IP control system looks like
- A signed NDA before files are shared. Not a promise to sign later. The document should cover confidentiality of drawings, moulds, tooling data, and the existence of the programme itself, with a stated duration.
- Restricted file access. Design files held on access-controlled storage, with named individuals granted access. Ask how access is granted and revoked when a staff member leaves.
- Physical segregation for sensitive projects. Where a programme is licence-critical, production of that item should be separated from general lines, with controlled entry.
- Scrap and reject handling. Defective moulded parts and rejected painted figures must be destroyed rather than sold on. Ask for the procedure.
- No use of your work in marketing without consent. Confirm that the manufacturer will not display your product, mould or sculpt in catalogues, exhibitions or social media without written approval. This is a common and easily overlooked leak channel.
| IP control | Question to ask | Adequate answer |
|---|---|---|
| NDA | Will you sign our NDA before we send files? | Yes, before any file transfer, with redlines acceptable |
| Access control | Who inside the company can open our sculpt files? | A named, limited list; access logged and revoked on departure |
| Subcontracting | Will any part of this project be subcontracted? | A clear yes/no, and if yes, which stages and under what NDA |
| Reject disposal | What happens to defective parts and rejected figures? | Documented destruction, ideally with photo evidence per batch |
| Marketing use | Will our product appear in your catalogue or online? | Only with written approval |
Dimension 5 — Capacity math, not capacity claims
"We have strong capacity" means nothing. Capacity is a calculation: machines × cavities × cycle time × shifts × working days, less changeover and tool maintenance. Ask the manufacturer to walk you through their arithmetic for a product family close to yours.
| Input | Typical question | Why it changes your decision |
|---|---|---|
| Machine count and tonnage | How many injection machines serve small-figure production? | Determines whether your tool gets dedicated press time or waits in a queue |
| Cavity count per tool | How many cavities does a figure of our size normally run? | Drives unit cost and the practical minimum order |
| Cycle time | What cycle time should we expect for our part weight? | The dominant term in both capacity and cost modelling |
| Shifts and days | How many shifts per day, how many days per week? | A single-shift operation has roughly a third of a three-shift output |
| Tool changeover loss | How much press time is lost to changeovers per week? | Large changeover loss erodes the theoretical capacity figure |
| Peak season behaviour | How do you allocate press time in your peak season? | Reveals whether your order will slip when their big customer calls |
The question that matters most: "If we place this order in your busiest month, what protects our slot?" A manufacturer with a real planning function will describe capacity reservation, a booking calendar, or a contractual slot commitment. A manufacturer without one will say they will "try their best" — which is not a plan.
Dimension 6 — Certification scope and test reports
Compliance is market-specific, and the applicable standard set depends on where the goods will be sold and to whom. A manufacturer should be able to name the relevant frameworks for your target market and produce reports issued by an accredited third-party laboratory.
| Market / concern | Commonly referenced frameworks | What the report must show |
|---|---|---|
| EU toy safety | EN 71 series (mechanical/physical, flammability, migration of certain elements) | Report number, accredited lab, model reference matching your product, issue date |
| US toy safety | ASTM F963 and CPSIA requirements including phthalate and lead limits | Same — plus confirmation the test article matches your BOM |
| EU chemicals | REACH SVHC and restricted substance obligations | Substance list tested and detection limits |
| Electrical / electronic content | RoHS where electronics or wiring are present | Restricted substance results by material |
| Packaging and labelling | Market-specific labelling, age grading, warnings, traceability marks | Artwork proof showing the final marks |
Three questions that expose weak compliance
- "Is the report issued against our exact model, or a family representative?" A report against a similar model does not automatically cover yours. Where a family approach is used, ask for the rationale and the BOM comparison.
- "Which laboratory issued it, and is that laboratory accredited for this test?" Report provenance matters as much as the result.
- "Does the report cover the paint and surface finish, or only the base material?" Migration and heavy-metal risk frequently sits in the coating, not the substrate. This is where incomplete testing most often shows up.
Practical note on who pays for testing: the cost of certification testing is normally a buyer cost, and the manufacturer arranges it. Establish up front which tests you require, whether sampling is included, and what happens to the cost if your product must be re-tested after a change. Agree this before tooling, not after first article.
Dimension 7 — Project management and reporting cadence
A custom figure programme runs for months and passes through several irreversible gates. The supplier's project management discipline determines whether you discover a problem at the gate or after mass production.
| Gate | What is being approved | What you should receive |
|---|---|---|
| Concept & brief freeze | Product definition, size, material direction, packaging format | A written brief restatement confirming mutual understanding |
| Sculpt review | Form, proportion, silhouette, feature accuracy | Six-view pack for markup and written approval |
| Structural / DFM review | Parting lines, wall thickness, undercut resolution, assembly logic | Annotated structural report with risks flagged |
| Prototype / white sample | Physical form, fit and function before tooling commitment | Physical sample plus a comparison note against the sculpt |
| Colour standard | Pantone or physical swatch approval, effect finishes | Approved colour sample retained by both parties as the reference |
| Tool trial / T1 sample | First parts from the production tool | T1 samples, dimensional report, deviation list |
| Pre-production sample | Parts from the tool in production conditions, decorated and assembled | PP sample for sign-off against the approved standard |
| Mass production & inspection | Volume output at the approved standard | In-process reports, AQL final report, pre-shipment report |
The single most useful management question: "Who is our named project contact, and how often will we receive a written status update?" Programme risk is usually not technical failure — it is a delay that nobody reported on time. A weekly written update with a status colour per gate gives you early warning at almost no cost to the manufacturer.
Scoring the seven dimensions
Use the table below as a working scorecard. Grade each dimension 0–2 and weight the structural dimensions more heavily. A total below 9 out of 14 indicates a supplier who needs supervision you should not be paying for.
| Dimension | Weight | Score 0 — not evidenced | Score 2 — fully evidenced |
|---|---|---|---|
| 1. Sculpting & engineering | ×2 | Outsourced, no native files, no six-view discipline | In-house sculptors, native files shared, formal six-view approval gates |
| 2. Tooling | ×2 | No register, ownership unclear, partner-cut | Machine list, mould register, cavity counts, buyer ownership documented |
| 3. QC | ×1.5 | Visual check only, no records | Staged checkpoints, AQL reports with arithmetic and defect classes |
| 4. IP | ×1.5 | Will "sign something later", no access policy | NDA first, named access list, scrap procedure, marketing-consent clause |
| 5. Capacity | ×1 | Adjectives only | Worked capacity arithmetic and a booking mechanism |
| 6. Compliance | ×1 | Undated or mismatched reports | Accredited reports against your model and BOM, coating included |
| 7. Project management | ×1 | No named contact, no cadence | Named PM, weekly written updates, documented gates |
Red flags that should stop the conversation
- Refusal to sign an NDA before file transfer. There is no legitimate reason to need your sculpt data before agreeing to confidentiality.
- No record of your design after the first meeting. A manufacturer receiving a technical brief should restate it back with questions. Silence means nobody has actually read it.
- Tooling ownership left unaddressed. If the question makes the supplier uncomfortable, the tool was never going to be yours.
- Price given before the design is understood. A credible price requires part weight, cavity count, material grade and decoration method. A number offered without those inputs is a guess.
- Willingness to skip certification testing. A supplier who suggests you can "probably" ship without the market-required test reports is transferring regulatory risk onto you.
- No answer on reject disposal. Uncontrolled rejects become grey-market product — and in licensed work, that becomes your problem.
- Constant change of contact. Repeatedly shifting account contacts usually signals a trading front end with no stable technical team behind it.
FAQ
How many custom toy manufacturers should I evaluate?
Evaluate three to five in the desk round and take two through a full factory review. Fewer than three removes your ability to benchmark pricing and reasoning; more than five consumes time without improving the decision, because the structural answers converge quickly.
Should I visit the factory?
For any programme involving significant tooling spend, yes — physically if practical, otherwise by a scheduled live video walkthrough with the camera moving through the tooling cell, moulding floor, painting line and QC area. Insist on seeing the areas you care about, and ask the operator to zoom in on the mould register or the QC station rather than at a showroom wall.
What is a reasonable sample and tooling lead time?
For a typical collectible figure, standard sampling commonly runs on the order of about a week depending on complexity, and tooling adds several further weeks before T1 samples exist. The specific figures vary with part count, undercut complexity and decoration. Ask for the schedule stage by stage and hold the milestones as gate dates rather than asking for one aggregate number.
Can I start with a smaller trial order?
Tooling economics usually set a practical floor, because the mould cost is fixed once cut. Where a supplier works with a minimum order band in the low thousands of units, a first order near the bottom of that band is the normal way to validate both the product and the relationship before committing to volume.
How do I verify claims without travelling to China?
Use a staged evidence path: NDA-signed technical exchange, native sculpt file screen-share, tooling register excerpt, a past AQL report, test reports with verifiable report numbers, and a scheduled live video walkthrough. Each step is cheap to provide for a genuine manufacturer and difficult to sustain for one that is not actually manufacturing.
Planning a custom figure programme?
Share your concept, target market and expected volume and we will come back with a structural view of the tooling approach, the compliance set your market requires, and a stage-by-stage schedule — before you commit to a tooling order.
Related reading — reading the numbers
Supplier vetting covers capability. When the shortlist is set, the next question is how to read the quotation you receive and which cost lines are genuinely negotiable.
Related reading — the schedule
A supplier can only be judged against the timeline you hold them to. See the eight stages of a custom toy order and which gates decide the final date.
Related reading
Once you have shortlisted suppliers, the next question is what a quotation should actually contain — and which cost lines are negotiable. See our breakdown of quotation structure and cost drivers.